

Spindle Bore Φ56, Φ66 or Φ82: How Thick a Bar Can You Actually Run?
Bottom line: spindle bore is the hole size, not the bar you can run. On this site the numbers group into four tiers: HMS-320MY bore Φ56 mm and rated bar Φ46 mm; HMS-550MY, HMS-550MYS and HMS-750 bore Φ65 mm and rated bar Φ52 mm; CK-6140 bore Φ66 mm; CK-6150B bore Φ82 mm. The two flat-bed lathes do not list a bar capacity, so confirm against the chuck and feeder configuration.
The most common selection error is treating bore as the bar limit. Between the hole and the bar sit chuck jaws, clamping margin and the feeder tube. Below, every bore figure is taken from the product specification tables on this site.
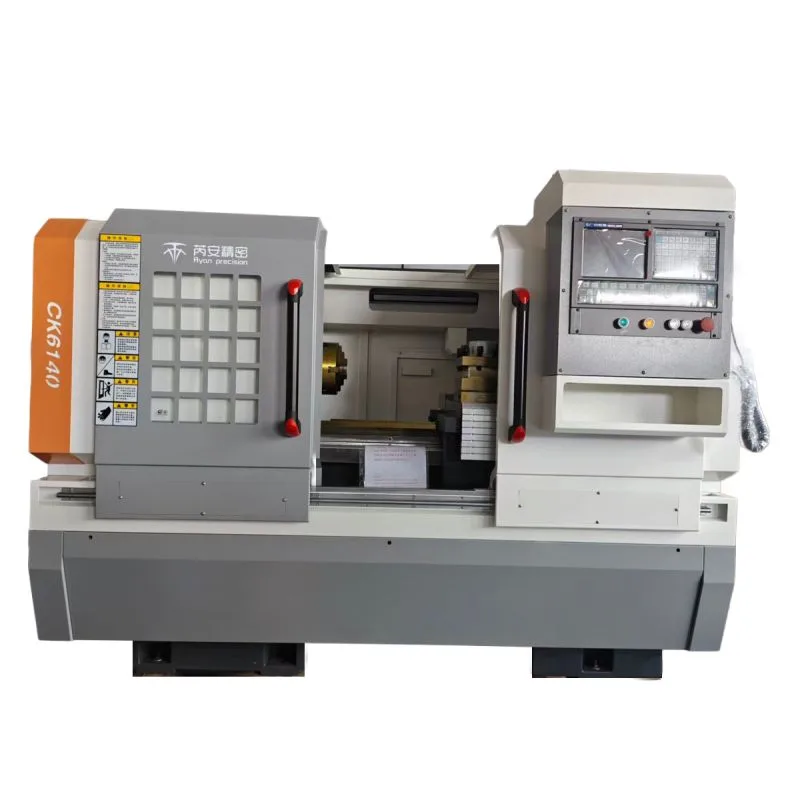
CK-6140
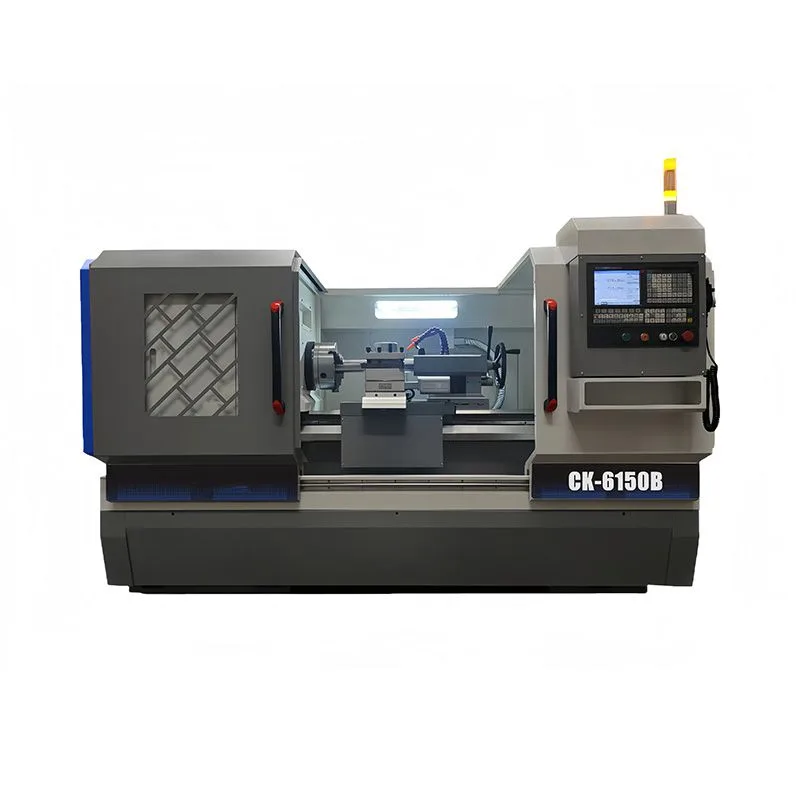
CK-6150B
Where does each bore size appear?
Φ56 mm appears on the HMS-320MY main spindle (A2-5, 4500 rpm, 6-inch chuck) and on the sub-spindles of the HMS-550MYS and HMS-750MYS (A2-5, 4000 rpm, 6-inch). Φ65 mm is the main channel of the HMS-550MY, HMS-550MYS and HMS-750 (A2-6, 4000 rpm, 8-inch). Φ66 mm is the CK-6140 (A2-6, 50–2000 rpm). Φ82 mm is the CK-6150B (A2-8, 65–1600 rpm).
| Machine | Spindle nose | Bore | Rated bar | Chuck / speed | Type |
|---|---|---|---|---|---|
| HMS-320MY | A2-5 | Φ56 mm | Φ46 mm | 6-inch / 4500 rpm | Turn-mill |
| HMS-550MY | A2-6 | Φ65 mm | Φ52 mm | 8-inch / 4000 rpm | Turn-mill |
| HMS-550MYS main / sub | A2-6 / A2-5 | Φ65 / Φ56 mm | Φ52 / Φ46 mm | 8-inch / 6-inch, 4000 rpm | Twin-spindle turn-mill |
| HMS-750 | A2-6 | Φ65 mm | Φ52 mm | 8-inch / 4000 rpm | Turn-mill |
| HMS-750MYS main / sub | A2-6 / A2-5 | Φ65 / Φ56 mm | Φ52 / Φ46 mm | 8-inch / 6-inch, 4000 rpm | Twin-spindle turn-mill |
| CK-6140 | A2-6 | Φ66 mm | not listed | servo stepless 50–2000 rpm | Flat-bed lathe |
| CK-6150B | A2-8 | Φ82 mm | not listed | geared 65–1600 rpm | Flat-bed lathe |
Why does a Φ65 mm bore only run Φ52 mm bar?
The 13 mm is not wasted. A bar must pass through the chuck jaw clamping zone, and the jaws need travel plus contact length; the bar itself has straightness and diameter tolerance. The margin is what keeps feeding smooth and stops the bar scoring the bore. 13 mm total is about 6.5 mm per side, a standard allowance.
On the HMS-320MY the difference is 10 mm, 5 mm per side, tighter because the compact spindle unit leaves less room. If a job needs bar close to Φ56 mm, the answer is a larger model, not a tighter chuck.
What does the CK-6140 do well?
Bed swing Φ420 mm, saddle swing Φ210 mm, centre distance 750 mm, A2-6 spindle, Φ66 mm bore, 50–2000 rpm servo stepless, tailstock sleeve Φ65 mm / stroke 150 mm / MT4. It is positioned for small and medium shaft, disc and general mechanical parts in batches, with a wide speed range for finishing and higher surface speeds.
For bar work, note that the site lists the bore only. Whether a Φ50 mm bar is viable depends on the chuck and feeder chosen, so confirm with the actual clamping setup rather than extrapolating from the bore.
Is the extra 16 mm on the CK-6150B worth it?
Compared with the CK-6140 the CK-6150B is one size up: bed swing Φ500 mm, saddle swing Φ290 mm, centre distance 1000 mm, A2-8 spindle, Φ82 mm bore, 65–1600 rpm geared three-step. It suits large shafts, tube parts and jobs that need a big boring bar or a mandrel through the spindle.
The trade-off is top speed. Large-bore spindles usually run slower, so small-diameter parts needing high surface speed lose out on the 6150B. The rule: large diameter, heavy stock, roughing and semi-finishing → 6150B; medium diameter, finishing, speed → 6140.
How do you size a bar in three steps?
Step one, bar OD below the bore — necessary, not sufficient. Step two, deduct the chuck clamping margin based on jaw travel and clamping length for the specific chuck. Step three, check the bar feeder tube, which is often the first limit in practice.
Only when all three pass is the size production-safe. Selecting on step one alone typically produces a machine that swallows the bar but cannot feed it reliably or clamp it long enough to avoid chatter.
Does a bigger bore cost rigidity or speed?
Within the same spindle nose size, a larger bore means thinner wall and less bearing space, and top speed usually drops. The site data shows the pattern: Φ66 mm at 2000 rpm on the CK-6140, Φ82 mm at 65–1600 rpm on the CK-6150B. Turn-mill spindles give up bore for C-axis hardware, which is why the HMS main channel stops at Φ56 and Φ65 mm.
Frequently asked questions
Q1: Is spindle bore the same as bar capacity?
A: No. The bore is a mechanical hole; bar capacity depends on chuck jaw travel, clamping length and the bar feeder tube. On this site the HMS-320MY has a Φ56 mm bore but a Φ46 mm bar capacity — the 10 mm difference is clamping margin.
Q2: Which machines use a Φ56 mm bore?
A: HMS-320MY: A2-5, Φ56 mm bore, 4500 rpm, 6-inch chuck, bar capacity Φ46 mm. The sub-spindles of HMS-550MYS and HMS-750MYS are also A2-5 with Φ56 mm bore, but they are the second spindle at Φ46 mm bar capacity, not the main channel.
Q3: What bar can a Φ65 mm bore machine run?
A: HMS-550MY, HMS-550MYS and HMS-750 all use an A2-6 spindle with Φ65 mm bore at 4000 rpm and 8-inch chuck, rated at Φ52 mm bar. The 13 mm difference covers jaw travel and clearance.
Q4: What is the CK-6140 suitable for?
A: CK-6140 is a flat-bed CNC lathe: bed swing Φ420 mm, saddle swing Φ210 mm, centre distance 750 mm, A2-6 spindle, Φ66 mm bore, 50–2000 rpm servo stepless, tailstock sleeve Φ65 mm / stroke 150 mm / MT4. It suits small and medium shaft and disc work in batches.
Q5: Does the extra 16 mm of the CK-6150B justify itself?
A: Only for the right parts. CK-6150B: bed swing Φ500 mm, saddle swing Φ290 mm, centre distance 1000 mm, A2-8 spindle, Φ82 mm bore, 65–1600 rpm geared three-step with stepless within each step. The larger bore passes larger stock and bigger boring bars, but the top speed is lower than the CK-6140's 2000 rpm.
Q6: How do I calculate the bar diameter for a machine?
A: Three checks: bar outside diameter below the bore; jaw travel and clamping length margin; bar feeder tube inside diameter, which is often the first real limit. All three must pass before the size is production-safe.
Q7: Does a larger bore reduce rigidity or speed?
A: In the same spindle nose size, a larger bore leaves less wall thickness and less bearing space, and top speed usually drops. The data here shows it: Φ66 mm bore at 2000 rpm on the CK-6140, Φ82 mm bore at 65–1600 rpm on the CK-6150B.
Q8: Why are turn-mill bores smaller than flat-bed lathes?
A: Turn-mill spindles carry C-axis indexing, a brake and live-tool interfaces, so the spindle unit is more compact. The HMS range main channel stops at Φ56 and Φ65 mm, while the flat-bed CK-6140 and CK-6150B reach Φ66 and Φ82 mm.
Dongguan Ruian Precision Machinery Co., Ltd.
Tel / WhatsApp: +86 13929438020 (Vince) Email: Vince@ruiancnc.com
Address: Floor 1, Building 7, No. 8 Tiankeng Gaoxin Road, Hengli Town, Dongguan, Guangdong, China
Website: ruiancnc.cn
Further reading
- HMS-320MY: which parts fit a compact turn-mill
- HMS-550MYS vs HMS-550MY: sub-spindle or tailstock
- HMS-320MY compact turn-mill specifications
- HMS-550MY specification
- CK-6140 specification
- CK-6150B specification
- All turn-mill and lathe articles
More specifications: HMS-550MYS, HMS-750, HMS-750MYS.
Next:
None
Related News
- -Spindle Bore Φ56, Φ66 or Φ82: How Thick a Bar Can You Actually Run?
2026-11-22 - -HMS-550MYS vs HMS-550MY: Sub-Spindle or Tailstock?
2026-11-22 - -HMS-320MY Compact Turn-Mill: Which Parts Actually Fit?
2026-11-22 - -What Does a ±50 mm Y-Axis Cover? HMS-750MY Turn-Mill Machine Explained
2026-11-21 - -Where Does the VMC-850L Get Its Rigidity? BT40, 35 N·m and Roller Guideways Explained
2026-11-21 - -QPR-46L vs QPR-36L: How to Choose a Gang-Tool Lathe (Bar Ø46 or Ø36)
2026-11-21 - -T600-5 5-Axis Machining Center: 10 Questions Buyers Ask Before Ordering
2026-11-20 - -How to Choose a 5-Axis Machining Center for Complex Parts
2026-11-19 - -CNC Turn-Mill Machine Manufacturer for Europe, Russia and South America
2026-11-18 - -HSK-A63 versus BT40: fixing the wrong comparison first, then what dual contact is actually worth
2026-11-16
